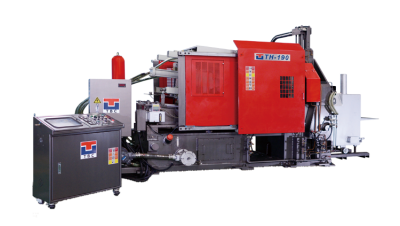
MÁY ĐÚC ÁP LỰC BUỒNG NÓNG
Máy đúc áp lực hợp kim kẽm chất lượng cao cho năng suất tối ưu
Hiệu suất chính xác, thiết kế thân thiện với người dùng
⚙️ Tương thích với hợp kim kẽm, magie và các hợp kim có nhiệt độ nóng chảy thấp
🔒 Độ ổn định và độ bền cao
🏗️ Thiết kế cơ khí ổn định
🖥️ Giao diện điều khiển thân thiện với người dùng
🤖 Vận hành và thao tác dễ dàng
💰 Giá thành cạnh tranh với chất lượng đạt tiêu chuẩn toàn cầu
Máy đúc áp lực buồng nóng hợp kim kẽm của TBC được thiết kế để mang lại độ chính xác, độ bền và tính dễ sử dụng. Chúng tôi cung cấp đa dạng mẫu máy nhằm đáp ứng nhu cầu của các nhà sản xuất trên toàn thế giới.
Với hoạt động nghiên cứu và phát triển liên tục cùng năng lực sản xuất tiên tiến, TBC mang đến các giải pháp đáng tin cậy và hiệu quả, giúp bạn tối ưu hóa quy trình đúc áp lực và giảm chi phí vận hành lâu dài.
- Controlled by Proportional solenoid valve
-Excellent in injection intensity
-Precisely control to enhance component quality
- Three-phase injection mechanism
-Provide low speed, high speed, and pressure retention
-Enhance air-tightness in pressure retention period

Controlled By Proportional Solenoid Valve
Three-phase Injection Mechanism
- Data Management
-Up to 250 sets of casting conditions able to be stored
-Enhance management efficiency
- Error message display
-Abnormal message for troubleshooting
- Three curves displayed in the figure: Pressure, Distance and Time
- Injection data will be displayed on the screen for further usage
- Proportional Solenoid Valve
-Smooth die close/open
-Short die close/open cycle
- Adjustable Sliding Shoes
-Adjustable platen height
-Keep movable platen in center position
- Freely switch between time/distance in low speed injection modes
- Effectively control the pressure and speed of injection with measured values provided
| Model | Units | TH-75 | TH-130 | TH-190 | TH-250 |
|---|---|---|---|---|---|
| Planten Part | |||||
| Die clamping force | ton | 75 | 130 | 190 | 250 |
| Tie bar diameter | mm | 60 | 75 | 90 | 110 |
| Die platen dimensions (HxV) | mm | 550 x 550 | 640 x 640 | 730 x 730 | 850 x 904 |
| Space between tie bars | mm | 329 x329 | 400 x 400 | 460 x 460 | 584 x 584 |
| Die stroke | mm | 210 | 310 | 350 | 380 |
| Die thickness | mm | 120~400 | 140~480 | 150~500 | 200~600 |
| Nozzle matching force | mm | 5.1 | 6.0 | 7.5 | 13.0 |
| Nozzle stroke | mm | 200 | 200 | 200 | 250 |
| Injection part | |||||
| Injection cylinder diameter | mm | 80 | 100 | 120 | 120 |
| Maximum injection force | ton | 5 | 7.85 | 10 | 12.5 |
| Maximum injection stroke | mm | 125 | 190 | 190 | 200 |
| Injector rod diameter (standard) | mm | 50 | 60 | 65 | 75 |
| Actual shot weight (zinc) | g | 1200 | 2500 | 3000 | 4500 |
| Furnace capacity (zinc) | mm | 0 , 60 | 0 , 80 | 0 , -100 | 0 , -150 |
| Maximum casting area | cm² | 253 | 494 | 615 | 929 |
| Casting pressure | kg/cm² | 256 | 200 | 238 | 269 |
| Ejection part | |||||
| Ejection force | ton | 5 | 6 | 7.5 | 10.5 |
| Ejection stroke | mm | 70 | 70 | 80 | 100 |
| Hydraulic part | |||||
| Operating pressure | kg/cm² | 110 | 110 | 110 | 125 |
| Accumulator (hydac) N2 (injection) | l/ea | 20 x 1 | 20 x 2 | 20 x 2 | 32 x 2 |
| Accumulator (hydac) N2 (die close) | l/ea | 10 x 1 | 20 x 1 | 32 x 1 | 50 x 2 |
| Oli tank capacity | l | 200 | 400 | 600 | 800 |
| Electrical part | |||||
| Electrical motor | kw | 11.0 | 15.0 | 18.5 | 30.0 |
| Machine size | |||||
| Machine weiht | ton | 5 | 7.5 | 10.5 | 14.7 |
| Machine size | m | 4.2x2.0x1.8 | 4.3x2.2x2.3 | 4.8x2.1x2.5 | 5.5x2.2x2.6 |